

Understanding plastic extrusion: processes, materials and industrial applications
At ABI Profils, we master single-screw and twin-screw extrusion, co-extrusion and post-extrusion to meet the most demanding specifications across multiple industries (construction, automotive, medical, aeronautics).
What is plastic extrusion?
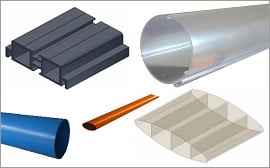
Plastic extrusion is a continuous process used to transform thermoplastic polymers. The raw material (granules, powders or resins) is melted and then pushed through a calibrated die to obtain a plastic tube or profile with precise dimensions.
The stages of the plastic extrusion process
1. Feeding the plastic material
The raw material (granules, powder or resin) is fed into an extruder equipped with a rotating screw.
The polymer is introduced into the hopper using gravimetric or volumetric feeders to ensure a perfectly consistent formulation.
2. Heating, plastification and melting
The single-screw or twin-screw system ensures progressive melting through controlled heating zones to achieve a homogeneous, workable melt.
- Temperature regulation via multi-point control
- Homogenisation through compression, dosing and degassing zones to eliminate bubbles or trapped air
3. Passage through the die
The molten polymer is then pushed under pressure through a die, which gives the product its final shape.
- The geometry of every die is optimised by our design office to stabilise melt flow and minimise shrinkage effects.
- Multi-channel dies can also be manufactured for co-extrusion to combine several materials (rigid/soft, transparent/opaque, etc.).
4. Cooling, calibration and dimensional stability
As it exits the die, the tube or profile is cooled and maintained in shape with calibrators, ensuring dimensional stability (final dimensions after cooling) and consistent mechanical properties.
5. Cutting and finishing
In-line or post-extrusion, we offer a full range of integrated finishing options:
- Automated straight or angled cutting
- Drilling, punching, threading according to specification
- Ink-jet marking for traceability, regulatory compliance or branding
- Application of technical adhesives (TESA, double-sided, repositionable) or magnets
At ABI Profils, the finishing department is integrated directly on site, in partnership with a Work Assistance Centre (CAT). This ensures responsiveness, flexible production and fully customised processing without external subcontracting.
Extrusion, co-extrusion and post-extrusion: what are the differences?
Traditional extrusion uses a single material. Co-extrusion, however, combines two or more polymers within a single profile, bringing together several properties such as rigidity and flexibility, or transparency and opacity.
Advantages of plastic co-extrusion
- Rigid/soft combinations (e.g. rigid PVC + soft SEBS)
- Bi-colour or bi-material components
- Enhanced technical performance (clipping strength, tightness, durability)
Example: an industrial sealing profile with a rigid base and a soft lip in SEBS or soft PVC.
Post-extrusion
Post-extrusion is an alternative technique in which a first section is extruded and stabilised before being reheated to integrate a second material through another die, generally a soft polymer.
Avantages de la post-extrusion plastique
- Optimal adhesion between materials
- Improved dimensional stability
- Great design flexibility for highly specific requirements
Example: industrial closure profiles—after extruding a rigid PVC section, it is reheated so that a soft lip (SEBS or soft PVC) can be added. This provides structural rigidity combined with air, water or sound tightness.
Which materials are used for plastic extrusion?
At ABI Profils, we work with a wide range of thermoplastic polymers selected for their technical properties and compatibility with the final application.
Comparative table of commonly used materials
| Material | Characteristics | Industrial applications |
|---|---|---|
| PVC (Polyvinyl Chloride) | Chemical resistance, rigidity, excellent value for money | Electrical tubes, technical profiles, sheaths |
| HDPE (High-Density Polyethylene) | Excellent impact and wear resistance | Food industry, chemical storage |
| PP (Polypropylene) | Lightweight, resistant to chemicals | Packaging, automotive, textiles |
| PA6 (Polyamide 6) | High mechanical and thermal resistance | High-performance components, aeronautics |
| SEBS (Styrene-Ethylene-Butylene-Styrene) | Elasticity and UV resistance | Sealing profiles, plastic straps |
Our experts will advise you on the most suitable material depending on your mechanical, chemical and thermal constraints.
ABI Profils: expertise and production capacity
Our expertise is supported by a high-performance, adaptable production system. We operate 15 single-screw and twin-screw extrusion lines and 6 co-extrusion lines, enabling us to offer tailor-made solutions for all industry requirements.
Our production capabilities
- Single-screw and twin-screw extrusion for high versatility
- Plastic co-extrusion for advanced bi-material components
- Custom manufacturing of plastic tubes and profiles
- Integrated ISO 9001 quality control
- Optimised production ensuring high repeatability and maximum dimensional accuracy
Thanks to this expertise, we support customers in diverse sectors: construction, industry, electronics, aeronautics, transport and medical.
Need an expert in plastic extrusion?
Looking for technical advice or a quotation? Get in touch with our teams to discuss your project and discover extrusion solutions tailored to your sector. Use our online contact form or call us on +33 4 71 61 29 99.
FAQ – Frequently asked questions
Extrusion shapes a single material, while co-extrusion combines multiple materials within one product to enhance mechanical and chemical properties.
Both processes combine several materials. Co-extrusion uses a multi-channel die, while post-extrusion requires a second, separate die to add an additional material after the first section is extruded.
Plastic extrusion is ideal for mass production of tubes and profiles with excellent dimensional precision, optimised production costs and great design flexibility.
The choice depends on the mechanical, chemical and thermal constraints of the final application. Our teams advise you on the most suitable option.
Cet article vous a intéressé ? Partagez le :
Nos autres actus
17 September 2025
ABI Profils strengthens its international team with the arrival of Else CARDEN
At ABI Profils, our commitment to international development is a core element of our growth strategy. As part of this ambition, we are pleased to announce the arrival of Else Carden within our sales team. Her international experience will be a valuable asset in supporting ABI Profils’ expansion across Europe.
17 September 2025
PVC Tubes or PP Tubes? Which performance for which application?
In many industrial sectors — from construction to food processing, as well as transport, chemicals and logistics — plastic tubes play a key functional role. Among the most commonly used materials, PVC (Polyvinyl Chloride) and PP (Polypropylene) stand out as leading solutions, each offering distinct technical advantages. Mechanical strength, chemical resistance, weight, cost, thermal behaviour, ease of processing: the choice between a PVC tube and a PP tube depends directly on the application’s technical constraints.
17 September 2025
PVC as a technical material: properties, advantages and industrial applications
PVC (Polyvinyl Chloride) is one of the most widely used thermoplastic polymers in the industrial world. Its versatility, durability and mechanical performance make it a key material for manufacturing technical tubes, profiles, mandrels and protective sheaths. Available in both rigid and flexible versions, PVC meets the requirements of various sectors such as construction, automotive, signage, packaging and medical.